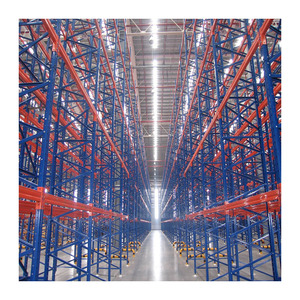
Industrial Pallet Rack
(1000-4000kg)
Robust industrial storage racks built for heavy loads, ensuring maximum stability and durability for demanding warehouse environments.
View Details
Discover a comprehensive range of custom OEM pallet rack shelving designed to optimize your storage capacity and operational efficiency. From heavy-duty industrial racks to specialized solutions, we deliver quality and performance.
Robust industrial storage racks built for heavy loads, ensuring maximum stability and durability for demanding warehouse environments.
View Details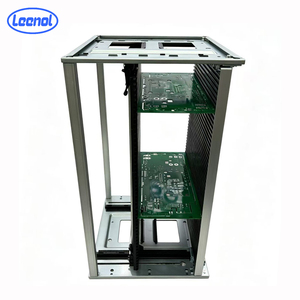
Custom-sized anti-static PCB storage racks designed for ESD-sensitive environments in electronics manufacturing, ensuring product integrity.
View Details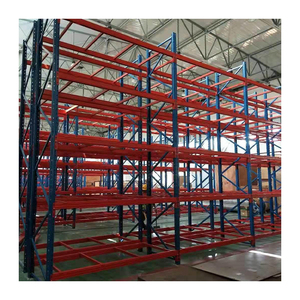
High-quality Q235 steel warehouse rack systems, expertly packed for export, ideal for fulfillment centers demanding reliability and efficient space utilization.
View Details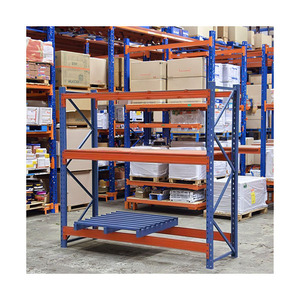
Stable, modular steel selective pallet racks with a 2000kg heavy-duty capacity, designed for distribution centers seeking efficient and secure storage.
View Details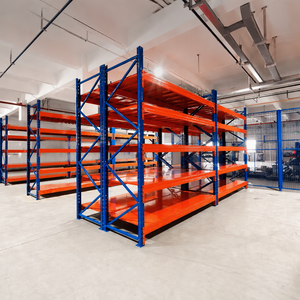
OEM/ODM adjustable heavy-duty industrial selective pallet racking shelving systems, offering flexibility and high-capacity storage for warehouses.
View Details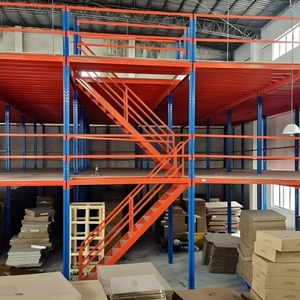
Heavy-duty mezzanine floor racking and storage rack shelf units, creating multi-level storage platforms to maximize vertical warehouse space.
View Details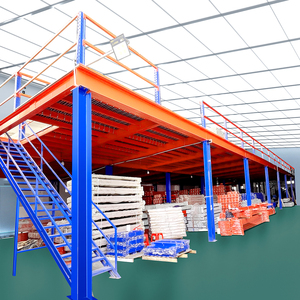
OEM multi-level heavy-duty industrial storage warehouse racks and pallet racking systems, including attic loft mezzanine floor platforms.
View Details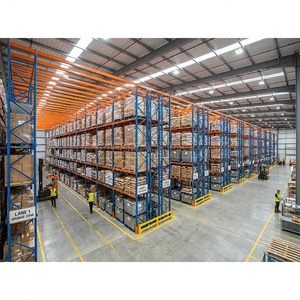
Heavy-duty drive-in pallet rack systems with 1000kg capacity, offering high-density storage with powder coating for enhanced durability.
View DetailsWe combine decades of manufacturing expertise with a commitment to global supply chain excellence. Our integrated approach ensures quality, compliance, and timely delivery for all your warehousing needs.
Tailored pallet rack shelving designed to your exact specifications, ensuring a perfect fit for your unique operational requirements.
Experienced in international shipping, ensuring secure packaging and timely delivery to distribution centers worldwide.
Utilizing premium-grade steel and robust construction techniques for maximum load capacity and extended product lifespan.
Adherence to international safety and quality standards, ensuring our pallet rack systems meet rigorous industry benchmarks.
As global supply chains evolve, warehouse managers and procurement specialists are looking for intelligent storage solutions that offer flexibility, sustainability, and smart integration.
The demand for pallet rack systems that can integrate with Warehouse Management Systems (WMS) and IoT sensors for real-time inventory tracking and performance monitoring is growing.
Manufacturers are increasingly focusing on using recycled steel and designing racks for easier disassembly and recycling at the end of their lifecycle.
The need for flexible storage solutions that can be easily reconfigured or expanded to adapt to changing inventory needs and warehouse layouts.
Increased emphasis on maximizing warehouse footprint through solutions like drive-in, push-back, and multi-level racking systems.
We are at the forefront of pallet rack development, constantly innovating to bring you safer, more efficient, and technologically advanced storage solutions for the modern warehouse.
Advancements in steel alloys and structural engineering allow for stronger, yet lighter, rack components, increasing load capacities while reducing material usage.
Ongoing research into base isolation technology and seismic bracing techniques ensures our racks perform exceptionally in earthquake-prone regions.
Introduction of advanced safety components like impact-resistant column protectors and user-friendly beam connections.
OEM (Original Equipment Manufacturer) pallet racks are storage solutions designed and manufactured by one company, then branded and sold by another. This allows businesses to offer custom-branded warehousing equipment without the overhead of manufacturing it themselves. We provide high-quality, custom-built pallet rack shelving under your brand.
Custom OEM pallet racking offers several advantages: **Brand Control:** You can brand the racks with your logo and colors. **Quality Assurance:** You leverage the expertise of an established manufacturer for reliable, high-performance products. **Cost Efficiency:** Often more cost-effective than in-house manufacturing. **Flexibility:** Racks can be precisely designed to meet specific load, dimension, and operational needs.
Our pallet rack shelving is primarily constructed from high-grade steel, such as Q235 and other structural steel grades, chosen for their exceptional strength, durability, and load-bearing capacity. Finishes often include powder coating for enhanced corrosion resistance and aesthetic appeal.
Selecting the right pallet rack depends on several factors: **Inventory Volume & SKU Count:** How many different items do you store? **Pallet Size & Weight:** What are the dimensions and weight of your typical loads? **Warehouse Layout & Aisle Width:** How much space do you have? **Product Rotation:** Do you need FIFO (First-In, First-Out) or LIFO (Last-In, First-Out) access? We offer various types including selective, drive-in, push-back, and flow racks. Our expert team can help you analyze your needs and recommend the optimal solution.
Lead times can vary based on the complexity of the customization, order volume, and current production schedules. Generally, custom OEM pallet rack orders can take anywhere from 4 to 10 weeks from design finalization to shipment. We provide an estimated lead time with each quotation.
While we manufacture and export pallet rack systems globally, we often work with certified installation partners in various regions. We provide detailed installation manuals and can connect you with qualified professionals to ensure your pallet rack system is installed safely and correctly according to engineering specifications.