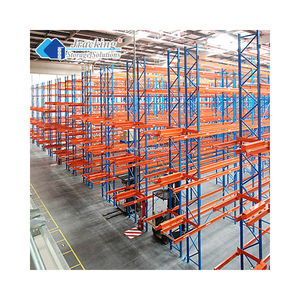
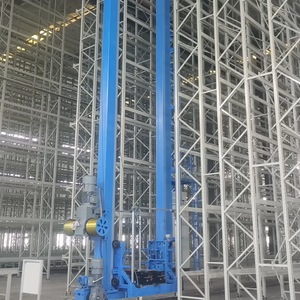
Global heavy-duty selective steel storage systems engineered for maximum load capacities, automated distribution centers, third-party logistics (3PL), and extreme seismic specifications.
Factory Direct Supply
High-Capacity Industrial Beam Pallet Racks
Explore engineered selective rack profiles precision-rolled from certified Q235B and high-yield structural steel, tailored for universal material handling, multi-tiered picking, and automated warehouse fulfillment.
Structural Mechanics of Heavy-Duty Beam Pallet Racking Systems
A rigorous examination of cold-formed roll forming, moment-resisting beam-to-column connections, and non-linear finite element structural simulations for international distribution centers.
Modern warehouse logistics mandates storage infrastructure that provides absolute operational reliability, maximum volumetric cubic utilization, and stringent compliance with building safety codes worldwide. Beam pallet racking—predominantly deployed as selective pallet racking—remains the fundamental architectural backbone for global supply chain distribution. As a premier original equipment manufacturer (OEM) and original design manufacturer (ODM), our production methodologies integrate automated roll-forming lines, automated laser-guided punching machines, and robotic continuous welding stations that calibrate cold-formed steel components to tolerances measured within fractions of a millimeter.
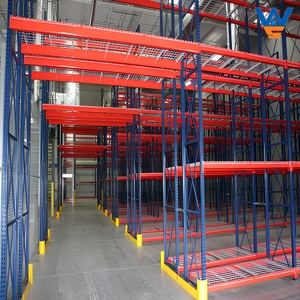
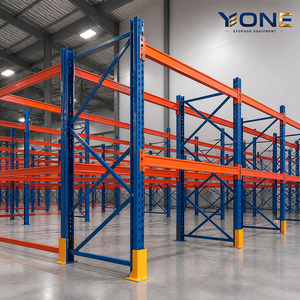
The structural integrity of a beam pallet racking system hinges on the synergistic interplay between two critical components: vertical upright frames and horizontal load-bearing beams. The upright frames, constructed with multi-bend cold-formed profiles (such as 6-bend and 8-bend omega sections), resist composite axial compression, lateral wind shear, and forklift collision dynamics. Horizontal beams—specifically interlocking box beams and step beams—are engineered with custom-machined end connectors containing 3, 4, or 5 integral claw hooks. These high-strength connectors transfer torsional moments into the upright column, significantly dampening longitudinal frame deflection and neutralizing systemic sway under seismic excitations.
Certified Metallurgy & Cold-Rolling
We strictly utilize certified hot-rolled coil (HRC) steel grades Q235B, Q355B, and ASTM A1011 structural steel. Continuous CNC roll forming with multi-pass tooling ensures residual stress reduction and uniform section thickness along the entire upright length.
Interlocking Robotic Seam Welding
Box beams are fabricated using twin C-sections continuous twin-welded along neutral axes via automated robotic MIG systems. Our fabrication facilities comply with CSA Standard W47.1 Division 3 for steel fusion welding and American Welding Society (AWS) standards.
Surface Pretreatment & Anti-Corrosion
A multi-stage chemical wash, iron-phosphate surface passivation, and automated electrostatic thermoset polyester powder coating guarantee a uniform 60–90 micron dry film thickness (DFT), passing 500-hour ASTM B117 salt spray environmental durability tests.
Strategic Procurement Insights
Emerging Procurement Trends in Pallet Racking (2025–2035)
How automation integration, decarbonized green steel procurement, and seismic resilience are transforming global corporate purchasing directives.
Trend 01
Automation & AGV/AMR Co-Design
Tier-1 procurement teams are transitioning from standard forklift layouts to automated guided vehicle (AGV) and autonomous mobile robot (AMR) compatible racking. This demands ultra-tight beam deflection limits (L/300 to L/400) and laser-calibrated runout tolerances to prevent sensor false-stops.
Trend 02
Decarbonized EPD & Green Steel
Global ESG directives are driving demand for Environmental Product Declarations (EPD). Wholesalers and enterprise buyers prioritize manufacturers utilizing Electric Arc Furnace (EAF) recycled scrap steel, cutting embedded carbon footprints by up to 60% compared to blast-furnace mills.
Trend 03
Advanced Seismic Base Isolation
High-risk seismic zones in North America, Australasia, and Europe necessitate active seismic dampening. Systems incorporating the Pellegrino Seismic Base Isolation System mechanically decouple rack uprights from ground ground motions, mitigating product spillage risks in critical hub facilities.
Trend 04
Modular Pitch Universal Hybridization
Multinational distributors increasingly request dual-pitch punching patterns (such as hybrid 50 mm / 76.2 mm or 2-inch teardrop profiles) to maintain interchangeability across decentralized geographic footprints, standardizing fleet maintenance and reducing spare part SKU bloat.
Data Visualization & Engineering Matrix
Structural Load Specifications & Design Criteria
Comprehensive engineering comparison across international connection styles, beam profiles, and deflection performance under ANSI MH16.1 and EN 15512 standards.
Profile Architecture
Connector Interface
Standard Pitch
Deflection Criteria
Maximum Bay Tonnage
Optimal Deployment
Teardrop Roll-Formed
Inverted Keyhole / Round Pin
50.8 mm (2.00 in)
L / 180 per ANSI MH16.1
12,000 – 18,000 kg
North America Standard / 3PL
Dexion 76.2 mm Metric
4-Claw Hook / Retaining Wedge
76.2 mm (3.00 in)
L / 200 per EN 15512
14,000 – 22,000 kg
Australasia, UK & Middle East
European 50 mm Adjustable
Multi-Tooth Spring Hook
50.0 mm Metric
L / 200 to L / 250
15,000 – 20,000 kg
Continental Europe / High SKU
Heavy Structural C-Channel
Grade 5 / Grade 8 Bolted Joint
76.2 mm or 100 mm
L / 240 Heavy Dynamic
22,000 – 35,000 kg
Freezer, Outdoor & Heavy Industry
High-Density VNA High-Bay
Tapered Hook / Rigid Moment-Lock
50 mm / 75 mm custom
L / 300 Automation Ready
20,000 – 28,000 kg
Turret Truck / ASRS Interface
Note: Actual structural load limits must be certified by professional engineers based on building slab geotechnical reports, concrete compressive strength (f'c ≥ 3,000 psi), and local seismic hazard spectral response accelerations (Ss, S1).
Enterprise Competitive Advantages
Why Tier-1 Wholesalers & Global EPCs Choose Our Factory
Combining world-class certifications, automated high-throughput production, and certified welding expertise to deliver unmatched manufacturing capability.
Triple RMI R-Mark Authorization
We are among the elite manufacturers holding complete RMI R-Mark certifications for Manufacturer, System Design, and Installation validation. Every manufactured component conforms strictly to ANSI MH16.1 standards, ensuring effortless municipal building permitting across North America.
CSA W47.1 & AWS Welding Certified
Certified in Division 3 of CSA Standard W47.1 for the fusion welding of structural steel via the Canadian Welding Bureau (CWB), supported by American Welding Society (AWS) certified welders. Every continuous box beam weld undergoes ultrasonic and destructive torsion testing.
OEM/ODM Customization Flexibility
From custom beam spans (from 1,000 mm up to 4,500 mm clear bay width) to proprietary upright punching geometries and custom brand powder coat color-matching (RAL codes), our engineering team transforms bespoke client CAD layouts into production-ready mill orders.
Proprietary Impact Protection
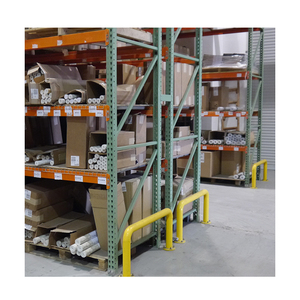
All upright configurations seamlessly integrate with engineered column guards and patented RAMGuard rubber-armored metal protectors, mitigating up to 85% of lower post deformation caused by reach truck outriggers and counterbalanced forklift impacts.
Comprehensive Seismic Calculations
Our dedicated structural engineering department provides site-specific stamped structural calculations, finite element modal analyses, and compatibility engineering with the Pellegrino Seismic Base Isolation System for high-risk zones across California, British Columbia, and earthquake-prone corridors.
Rapid Quick-Ship Fulfillment Hubs
Strategic stocking distribution centers maintain extensive inventories of industry-standard roll-formed uprights, universal step beams, wire decking, and row spacers, facilitating 48-to-72 hour emergency turnarounds for fast-track warehouse expansions.
Procurement Knowledge Base
Frequently Asked Questions: Global Pallet Rack Procurement
Detailed technical, commercial, and regulatory answers addressing the primary evaluation criteria of industrial warehouse procurement directors.
What engineering standards govern your beam pallet racking design and manufacture?
Our pallet rack systems are engineered in strict compliance with the Rack Manufacturers Institute (RMI) Specification ANSI MH16.1: "Design, Testing and Utilization of Industrial Steel Storage Racks," European Standard EN 15512: "Steel static storage systems – Adjustable pallet racking systems – Principles for structural design," and Australian Standard AS 4084-2023. Our production facilities maintain ISO 9001:2015 quality management certifications and are certified under CSA W47.1 Division 3 by the Canadian Welding Bureau.
What is the allowable beam deflection limit for selective pallet racking?
Under ANSI MH16.1 section 5.3, the maximum vertical deflection of a pallet rack beam under design uniform distributed load (UDL) cannot exceed L/180 (where L is the clear span distance between upright columns). For sensitive automated warehousing, AS/RS setups, or automated guide cart interfaces, our OEM design can be specified to L/200, L/240, or L/300 to minimize robotic positioning errors and laser sensor obstructions.
How do you ensure seismic compliance for facilities in active seismic zones?
Seismic rack design is governed by the International Building Code (IBC) and ASCE 7 Chapter 15. Our structural engineers utilize site-specific latitude and longitude to determine mapped spectral accelerations (Ss, S1) and Site Class soil amplification factors. We engineer widened heavy-gauge baseplates (up to 12 mm or 16 mm thickness), high-capacity wedge or screw anchors, heavy horizontal/diagonal bracing channels, and, where ground motion is severe, incorporate the patented Pellegrino Seismic Base Isolation System to dissipate earthquake energy before it transfers into the structural frame.
What is the difference between roll-formed teardrop and structural steel pallet racks?
Roll-formed teardrop rack is cold-rolled from high-strength coil steel (typically 1.5 mm to 2.5 mm thickness), featuring a keyhole punch pattern that allows toolless, boltless beam installation with integrated gravity safety pins. It is cost-effective, versatile, and the dominant standard across North America. Structural rack is fabricated from hot-rolled C-channel structural steel with bolted beam-to-column connections. Structural racks offer significantly higher impact resistance against heavy forklifts, making them ideal for high-throughput food distribution, cold-storage freezers (-30°C), and harsh outdoor yard storage.
What anti-corrosion finishes are available for harsh or cold-chain environments?
We provide three distinct surface treatments based on environmental exposure: (1) Standard Automated Electrostatic Polyester Powder Coating: Ideal for ambient climate-controlled facilities, providing superior scratch resistance and UV stability. (2) Hot-Dip Galvanization (HDG): Engineered per ASTM A123 / ISO 1461, immersing the fabricated steel in molten zinc to form a metallurgical iron-zinc alloy layer with unmatched corrosion resistance for outdoor, coastal, and chemical facilities. (3) Pre-Galvanized Coil Forming: Utilizing continuous zinc-coated steel coils for cost-effective protection in sub-zero cold-storage facilities and humid condensation zones.
How does your factory accommodate OEM custom branding and distributor private labeling?
As a full-scope OEM/ODM partner, we provide complete custom private-label services for regional wholesalers and racking distributors. This includes customized upright hole punch profiles (Teardrop, Dexion 76.2 mm, European 50 mm, or custom slotted), embossed company logos on connector safety clips or baseplates, tailored RAL color combinations for corporate branding, custom branded load capacity warning plaques, and customized export packing crates designed for container unloading efficiency.
How do you optimize container loading to prevent transit damage during international export?
Beam pallet rack components are heavy, dense, and high-volume. Our export logistics team utilizes 3D container packing simulation software to achieve 98%+ volumetric and weight optimization inside 40ft High Cube (HQ) containers. Beams are stacked in custom interlocking bundles with steel strapping, heavy-duty cardboard edge protectors, and wooden dunnage spacers to facilitate smooth forklift fork entry. Upright frames are either shipped knock-down (unbolted) to save ocean freight cubage or pre-assembled in custom welded cradles to match local job-site crane capabilities.
Ready to Engineer Your Optimal Storage Infrastructure?
Connect with our structural engineers and wholesale sales team to obtain site-specific load calculations, custom OEM/ODM roll-forming specifications, and competitive factory-direct wholesale pricing.