Strategic Overview: Why Choose Our Racking Systems for the US Market
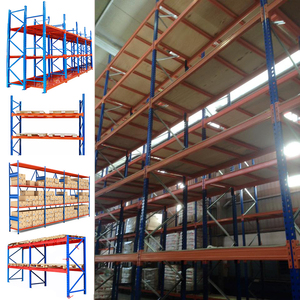
In the evolving landscape of North American logistics, the demand for high-efficiency storage has never been greater. As a premier manufacturer and exporter, we provide industry-leading mobile shelving and pallet racking systems designed to maximize cubic storage volume while ensuring structural integrity compliant with ANSI MH16.1 standards.
Local Application Scenarios
Our systems are engineered for diverse environments, ranging from high-velocity e-commerce fulfillment centers in California to temperature-controlled cold storage facilities in the Midwest. By integrating anti-corrosion safety designs and heavy-duty seismic bracing, we address the specific operational challenges faced by US-based logistics partners.
Trends Shaping the US Warehouse Market
Modern US warehousing is shifting toward High-Density Automation. Our modular mezzanine systems and gravity-fed racking are at the forefront of this trend, allowing businesses to scale operations without the need for additional square footage. We prioritize "Information Gain" by offering consultative design services that help clients navigate fluctuating real estate costs and labor shortages through smarter spatial management.
Commonly Asked Questions (FAQ)
Q: Are your racking systems compliant with US building codes?
A: Yes, our engineering team ensures all exported systems meet or exceed local safety requirements, including seismic load calculations.
Q: How do you handle shipping to the United States?
A: We utilize robust logistics networks to provide end-to-end support, ensuring timely delivery and minimal installation downtime.
Q: Can you customize systems for specialized goods?
A: Absolutely. From chemical-resistant coatings to specific weight-bearing capacities for heavy machinery, we offer tailored manufacturing solutions.
Our Commitment to Excellence
We leverage decades of manufacturing expertise to bridge the gap between high-quality Chinese engineering and American distribution needs. Our commitment to the E-E-A-T principle ensures that every rack we ship is supported by rigorous testing, transparent documentation, and a dedicated US-facing technical support team.